
Blog
The Ultimate Clinic Guide to Managing Precision Machining Partners Across Jiangsu Province: Efficacy, Wavelengths, and ROI
2026年9月23日
Why Jiangsu Province Is the Strategic Epicenter for Medical Aesthetic Device Precision Machining
For clinic owners and device brand managers, the reliability of a medical aesthetic laser platform is not determined in the treatment room—it is determined long before the device ships, at the precision machining partner level. Jiangsu Province has emerged as one of the most concentrated and mature ecosystems for medical aesthetic device manufacturing, owing to its dense network of CNC machining suppliers, optical component specialists, and ISO 13485-certified contract manufacturers. This guide, written from 15 years of B2B aesthetic device procurement and clinical consulting experience, provides a rigorous framework for evaluating, qualifying, and managing precision machining partners across Jiangsu’s industrial clusters—Suzhou, Wuxi, Changzhou, Nanjing, and Nantong.
Unlike generic consumer electronics supply chains, aesthetic laser systems demand machining tolerances in the ±5 to ±20 micron range for handpiece assemblies, water-cooling manifolds, and laser bar mounting blocks. A deviation of even 10 microns in the thermal interface of an 808nm diode laser stack can raise junction temperature, reduce energy density (fluence) stability, and ultimately degrade clinical outcomes in selective photothermolysis.
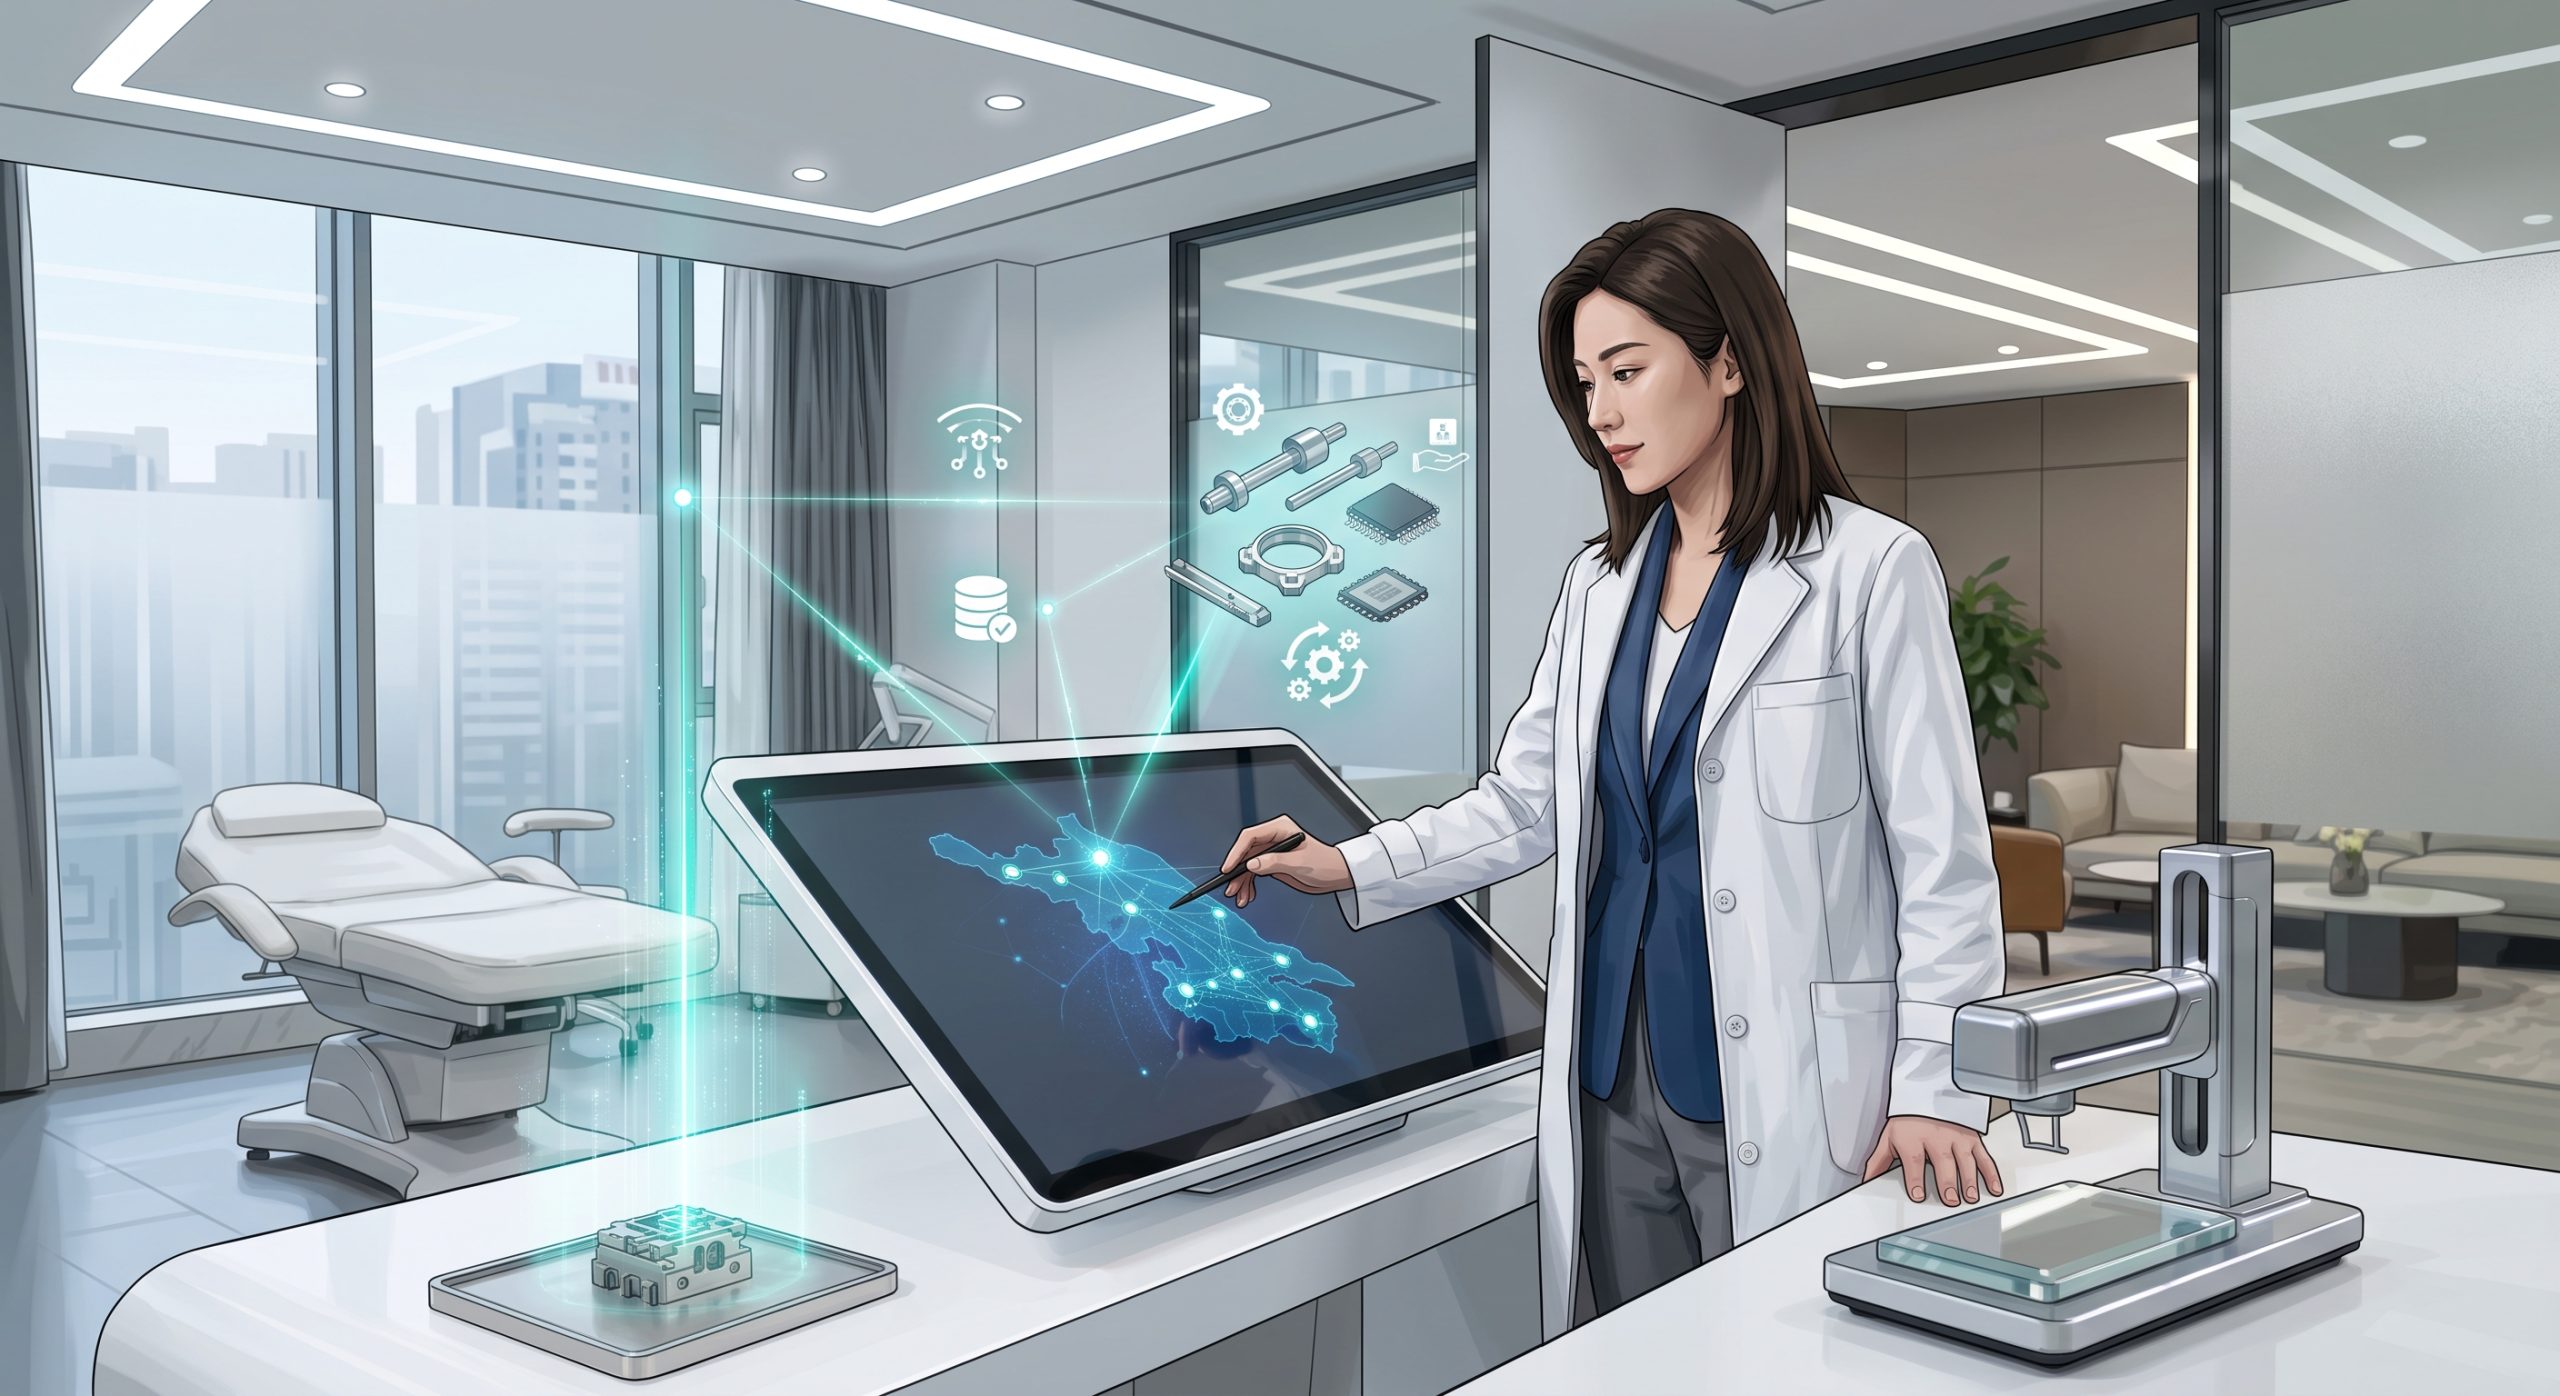
The Physical Mechanism: Why Machining Precision Directly Governs Clinical Efficacy
From Metal Tolerance to Tissue Interaction
Every clinical parameter your operators rely on—755nm, 808nm, and 1064nm wavelengths, spot size (typically 10x10mm to 20x20mm for diode platforms), pulse width (10ms–400ms), and fluence (10–120 J/cm²)—is ultimately a downstream expression of mechanical precision. The laser bar must be mounted with sub-micron flatness to ensure uniform emitter-to-emitter output. The sapphire cooling window must be lapped and polished to maintain thermal contact without optical distortion.
When a precision machining partner in Jiangsu fails to hold flatness or surface roughness (Ra) specifications, the clinical consequences are measurable: uneven fluence distribution across the spot, hot spots that increase epidermal injury risk, and shortened handpiece shot lifespan. This is why procurement audits must examine machining capability as a clinical risk factor, not merely a cost variable.
Critical Machining Tolerances for Aesthetic Laser Sub-Assemblies
- Laser bar mounting block: Flatness ≤ 2 µm, parallelism ≤ 5 µm, surface roughness Ra ≤ 0.2 µm
- Sapphire contact cooling housing: Concentricity ≤ 10 µm, leak-tightness verified at 1.5x operating pressure
- Water-cooling manifold: Internal channel burr-free, flow variance ≤ 5% across channels
- Handpiece optical bench: Angular alignment ≤ 0.05°, positional tolerance ≤ 15 µm
These are not aspirational figures. They reflect the specifications routinely achieved by top-tier Jiangsu machining suppliers serving Medical CE and FDA-cleared platforms. Clinics and OEMs that accept looser tolerances inherit hidden clinical and warranty risk.
Technical Specifications: Benchmark Parameters for Jiangsu-Sourced Aesthetic Laser Platforms
The following table consolidates the core technical and machining-linked specifications that should be verified when managing a Jiangsu precision machining partner. These values represent current industry benchmarks for high-throughput diode and solid-state aesthetic platforms.
| Key Parameter | Technical Specification |
|---|---|
| Wavelength / Laser Type | 755nm / 808nm / 1064nm Diode or Alexandrite-Diode Hybrid |
| Spot Size | 10x10mm to 20x20mm (typical), ±5% uniformity |
| Energy Density / Fluence | 10–120 J/cm², adjustable in 1 J/cm² increments |
| Pulse Width | 10ms–400ms, dependent on wavelength and indication |
| Repetition Rate | 1–10 Hz |
| Cooling System | Sapphire Contact Cooling (0–5°C) with TEC assist |
| Handpiece Shot Lifespan | 20–50 million shots (benchmark) |
| Machining Tolerance (Critical Parts) | ±5 to ±20 microns |
| Quality Certification | ISO 13485, Medical CE, FDA Clearance (platform-level) |
| Chassis Material | 6061-T6 Aluminum / 316L Stainless Steel |
| Water Cooling Circuit | Burr-free manifold, flow variance ≤5% |
Qualifying Jiangsu Precision Machining Partners: A Due-Diligence Protocol
Certification and Quality System Verification
Jiangsu hosts hundreds of machining workshops, but only a minority are genuinely qualified for medical aesthetic device production. The first filter is ISO 13485 certification—not merely ISO 9001. ISO 13485 imposes device-specific requirements for traceability, process validation, and risk management that directly affect patient safety. Additional verification should include Medical CE technical file support and, for U.S. market devices, evidence of FDA clearance pathways for the finished platform.
On-Site Audit Priorities
- CNC and turning capability: 5-axis machining centers, Swiss-type lathes, and in-house metrology (CMM, optical comparators)
- Cleanroom assembly: Class 10,000 or better for optical sub-assemblies
- Process validation: IQ/OQ/PQ documentation for critical machining processes
- Traceability: Material certificates (e.g., 6061-T6 aluminum, 316L stainless steel, oxygen-free copper) linked to lot numbers
- Change control: Notification obligations for any process, material, or sub-supplier change
Partners who resist on-site audits or cannot produce process validation records should be disqualified regardless of price. In aesthetic devices, unverified machining quality translates directly into inconsistent fluence delivery and elevated complication rates.
Clinical Implications: Fitzpatrick Skin Types and Wavelength Selection
Machining quality affects all wavelengths, but its clinical visibility is most pronounced in multi-wavelength platforms. A platform combining 755nm, 808nm, and 1064nm relies on precise optical alignment to switch between wavelengths without realignment drift. When the handpiece optical bench is machined to tolerance, operators can safely treat Fitzpatrick Skin Types I–VI with appropriate parameter selection:
- Types I–II: 755nm or 808nm, lower fluence, shorter pulse widths for pigment and hair removal
- Types III–IV: 808nm or 1064nm, moderate fluence, longer pulse widths for vascular and hair reduction
- Types V–VI: 1064nm preferred, conservative fluence, extended pulse widths, aggressive sapphire contact cooling
If the machining partner cannot guarantee consistent spot size and beam uniformity, the clinic cannot safely push parameters for higher Fitzpatrick types—limiting the device’s commercial versatility and patient throughput.
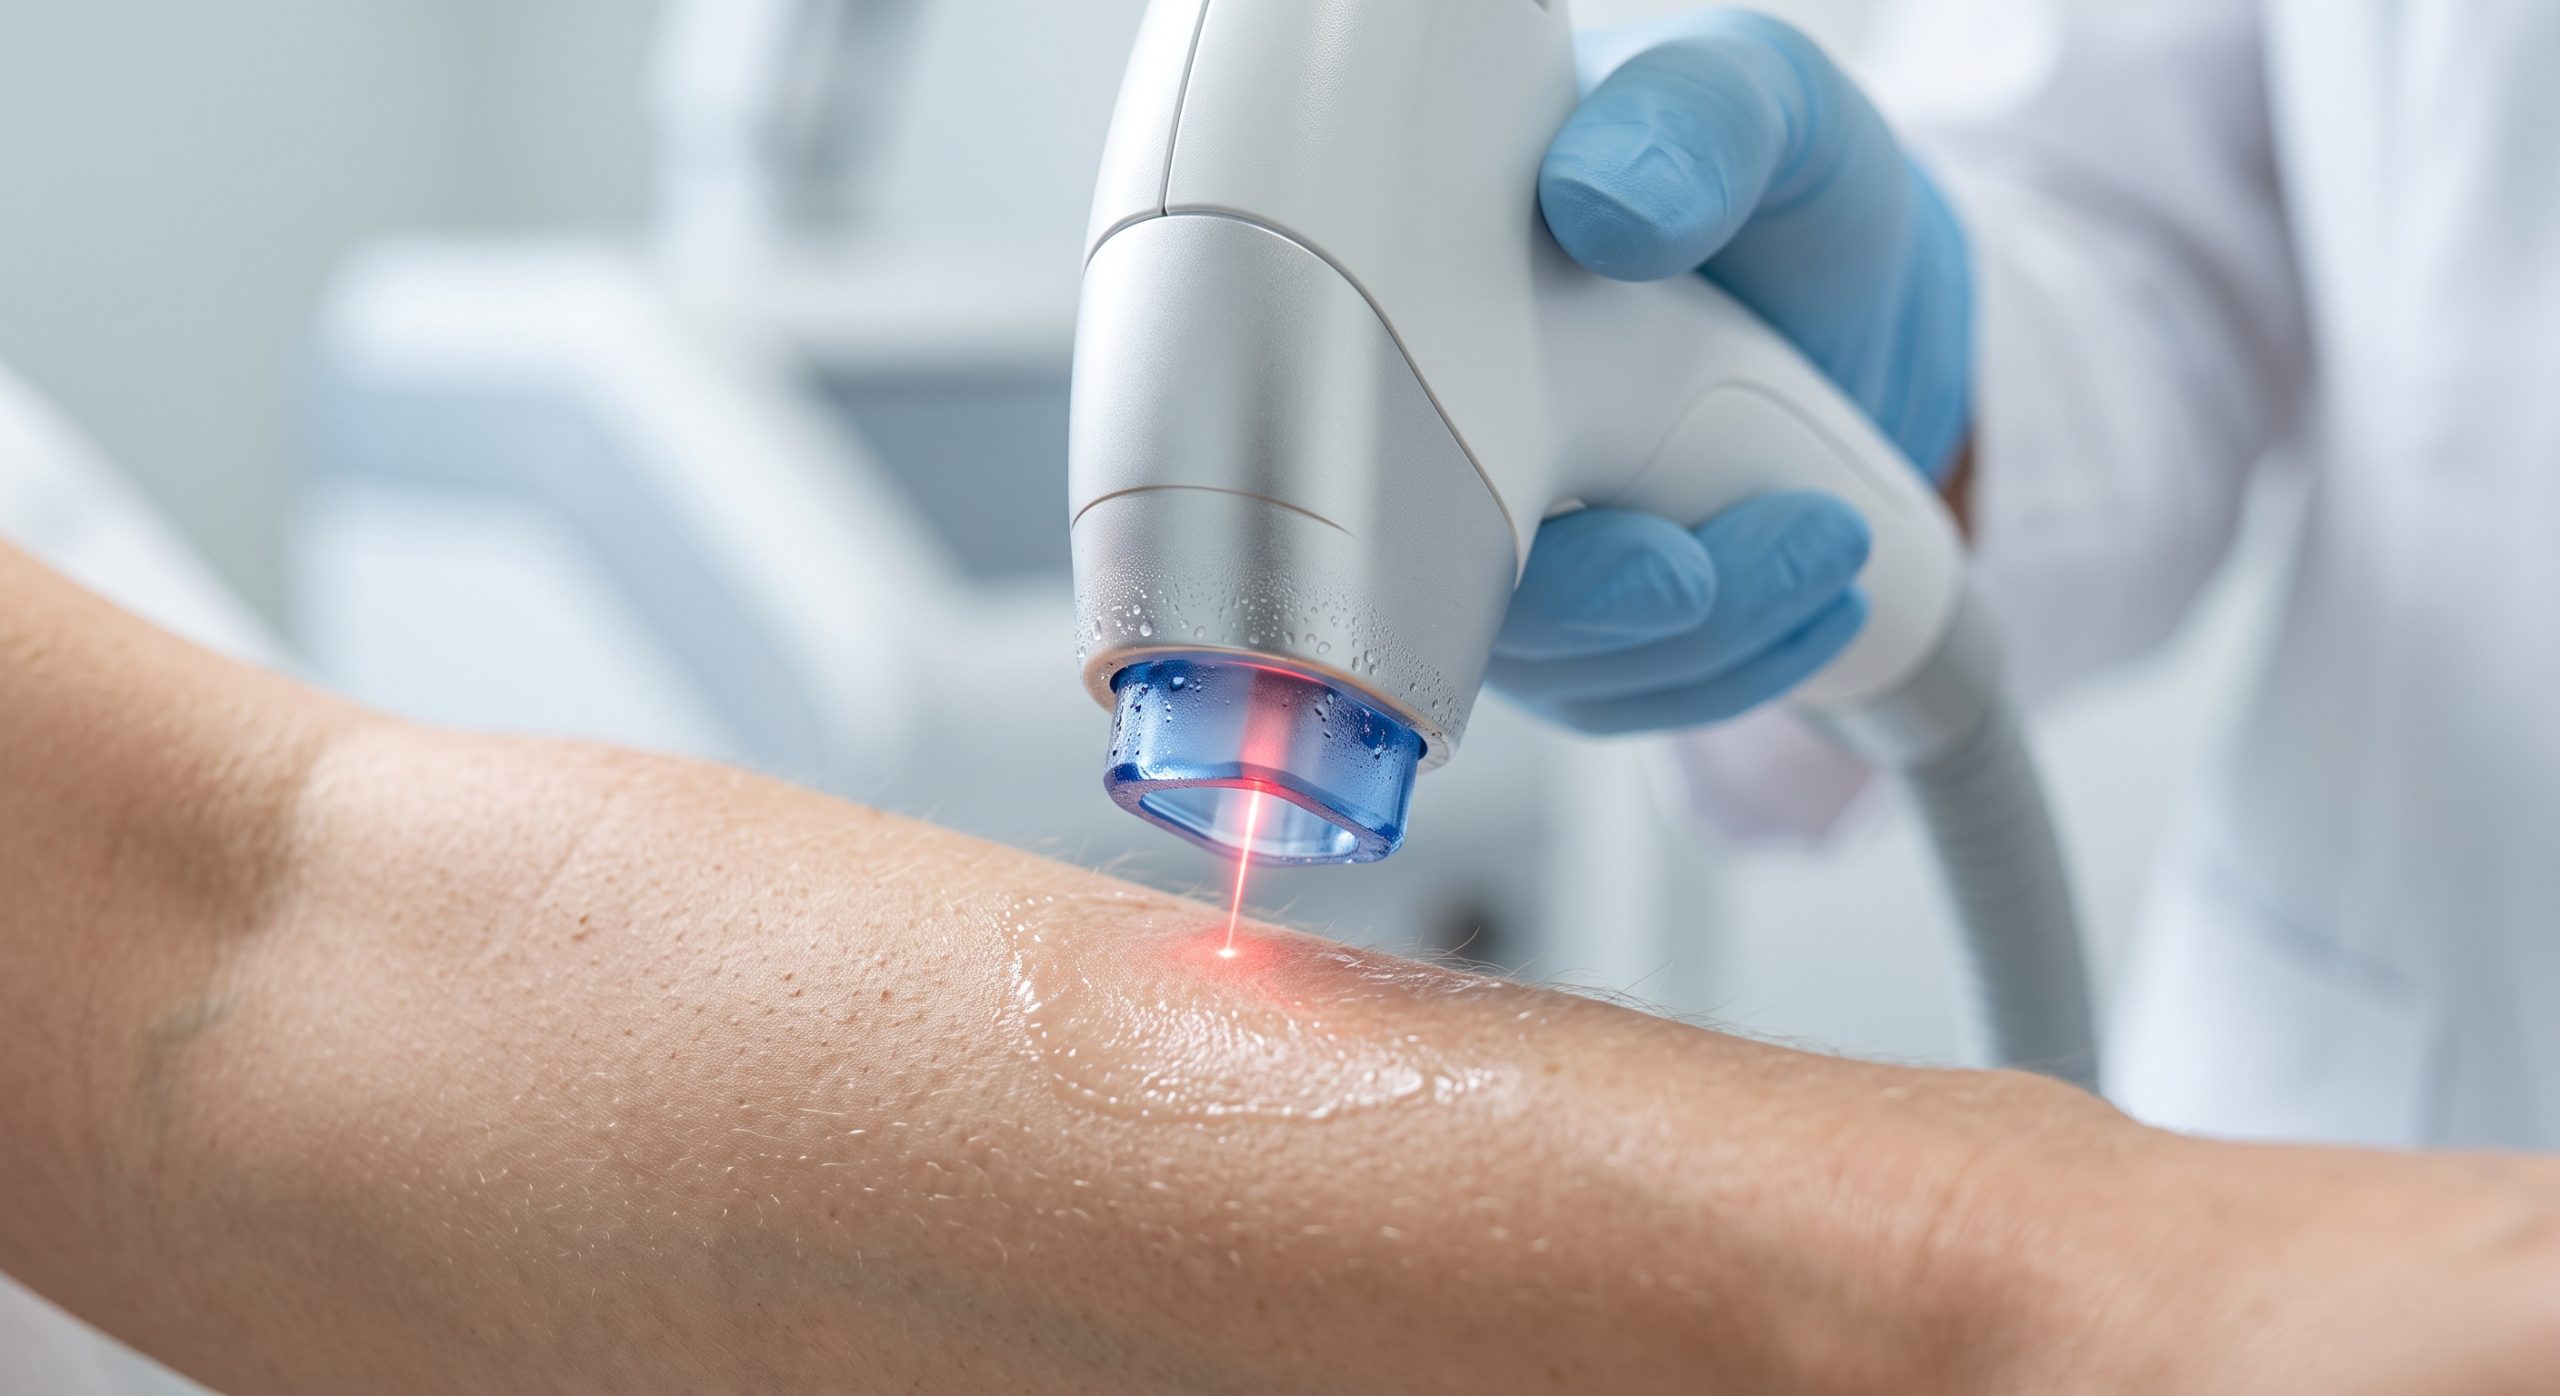
ROI, Total Cost of Ownership, and Strategic Partner Management
Consumables and Handpiece Durability
The handpiece shot lifespan is one of the most underappreciated ROI variables in aesthetic laser procurement. A poorly machined laser bar mount accelerates thermal degradation, reducing shot count from a benchmark 20–50 million shots to as low as 5–10 million. At a consumable cost of $3,000–$8,000 per handpiece replacement, this difference can swing annual operating profit by tens of thousands of dollars per device.
Throughput and Revenue per Hour
Precision machining also enables larger spot sizes (e.g., 20x20mm) and higher repetition rates (up to 10Hz), which directly reduce treatment time. For high-volume med spas, a platform that reduces a back treatment from 20 minutes to 12 minutes can increase daily patient capacity by 30–40%, translating into significant revenue acceleration.
Managing the Partner Relationship
- Dual-source critical components: Qualify at least two Jiangsu machining partners for handpiece and cooling assemblies
- Contractual quality gates: Define AQL sampling, first-article inspection, and PPAP-style submission requirements
- Escalation and remediation: Establish clear CAPA timelines and financial remedies for non-conformance
- Intellectual property protection: Execute NDAs and design-for-manufacture agreements before sharing CAD files
Jiangsu’s machining ecosystem offers world-class capability, but it rewards buyers who manage it with clinical-grade rigor. The difference between a profitable, compliant aesthetic laser platform and a liability often comes down to the discipline applied to partner qualification and ongoing quality management.
Conclusion: Precision Machining as a Clinical and Commercial Imperative
Managing precision machining partners across Jiangsu Province is not a back-office procurement task—it is a clinical governance responsibility. The wavelength accuracy, fluence stability, spot size consistency, and cooling efficiency that define patient safety and treatment efficacy all trace back to machining tolerance. By applying the audit protocol, specification benchmarks, and partner management practices outlined in this guide, clinic owners and device brands can secure reliable, Medical CE and FDA-compliant platforms while protecting margins and patient outcomes. In the competitive B2B medical aesthetic landscape, the organizations that treat machining precision as a strategic asset will consistently outperform those that treat it as a commodity.